Views: 0 Author: Site Editor Publish Time: 2026-08-31 Origin: Site


Modern fabrication shops face escalating costs for high-value raw materials. Tooling wear and complex machining setups routinely eat away at profit margins. Production engineers and shop managers constantly battle these daily inefficiencies. The central dilemma becomes quite clear. Can transitioning to a Waterjet Cutting Machine truly replace traditional CNC milling? Alternatively, does this equipment serve merely as a supplementary roughing process?
We will provide a clear, evidence-based evaluation of both manufacturing methods. You will discover exactly where abrasive waterjets outperform traditional milling. You will also learn where they fall short in precision applications. Finally, we will guide you through calculating the true return on investment for your production line. Understanding these critical trade-offs ensures you make profitable equipment investments. Making the right choice ultimately streamlines your entire shop floor operations.
No Heat-Affected Zone (HAZ): Waterjet cutting is a cold process, eliminating thermal distortion and secondary annealing steps required by heat-generating machining.
Superior Material Utilization: Tighter nesting and a narrow kerf significantly reduce expensive raw material waste compared to wide-diameter end mills.
Geometric Limitations: While ideal for 2D and 2.5D through-cuts, waterjets cannot match the blind-pocketing, threading, and 3D surface machining capabilities of a multi-axis CNC mill.
Operating Cost Realities: Abrasive consumption and high-pressure pump maintenance are strict ongoing costs that must be factored into part-cost comparisons.
Traditional milling removes material through mechanical shear. This physical action relies on rigid setups and expensive consumable cutting tools. Over time, these dependencies create significant production bottlenecks. You must identify these inefficiencies to understand where alternative cutting methods provide value.
Machining work-hardening metals destroys cutting tools quickly. Alloys like Titanium Grade 5 and Inconel 718 generate extreme localized heat during milling. This heat hardens the material ahead of the cutter. Abrasive composites like Carbon Fiber or G10 also cause exponential carbide tool wear. Shops spend thousands of dollars monthly replacing worn end mills. This tooling attrition heavily inflates the final cost per part.
Setup times introduce massive amounts of non-billable hours. Machinists spend excessive time designing complex workholding solutions. They frequently cut custom soft jaws for irregular parts. Multi-operation setups require operators to flip parts repeatedly. Each flip introduces a chance for human error. It also demands fresh dial indications and work offset adjustments. This downtime halts spindle rotation and stops revenue generation.
Material yield inefficiencies present another major financial drain. Traditional chip-making inherently turns high-value raw material into low-value swarf. You cannot tightly nest milled parts on a standard fixture block. Machinists must leave wide clamping margins to hold the stock securely. They also need extra space for wide end mills to clear the part boundaries. This wastes expensive alloys.
Common Milling Mistakes:
Over-specifying tolerances on non-critical features, driving up cycle times.
Ignoring the high cost of material scrap when quoting titanium or aerospace alloys.
Underestimating the labor hours spent programming multi-sided setups.
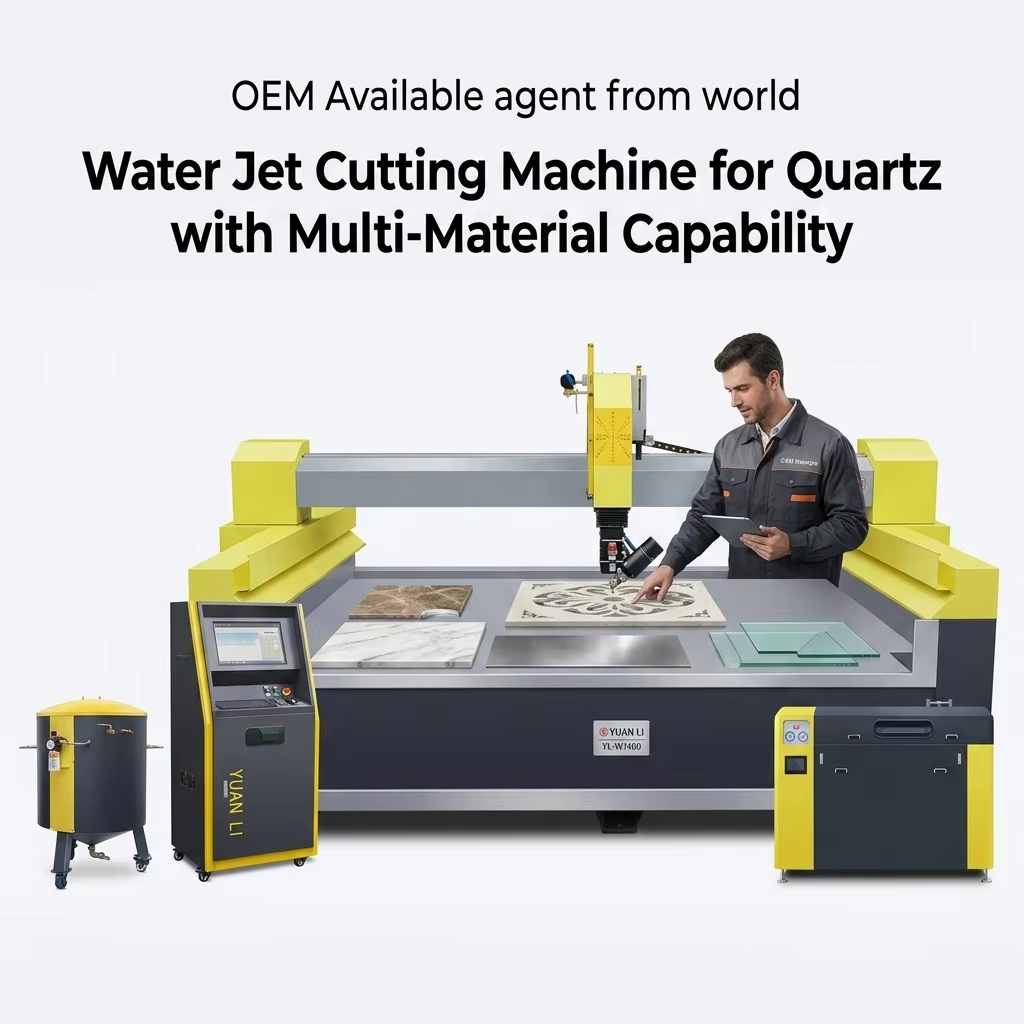
Understanding the fundamental mechanics of a Waterjet Cutting Machine clarifies its unique advantages. The process relies on extreme pressure rather than mechanical shear. High-pressure intensifier pumps force water through a tiny jewel orifice. This creates a supersonic stream capable of severing thick materials.
The cold cutting paradigm defines this technology. A pure water stream handles soft materials like foam or rubber. For metals, operators use an abrasive waterjet (AWJ) process. The machine pulls garnet abrasive into the mixing tube. The stream fires at 60,000 to 90,000 PSI. Because it operates at room temperature, it causes no thermal degradation. This eliminates the Heat-Affected Zone (HAZ) entirely.
Omni-directional cutting changes how programmers approach toolpaths. A mill relies on spindle rotation and cutter radius. A waterjet stream acts like a microscopic band saw. It allows for incredibly sharp internal corners. The sharpness depends only on the narrow kerf width. The machine cuts any 2D vector path without ever requiring a tool-change interruption. They follow complex geometric contours seamlessly.
Material agnosticism makes these machines incredibly versatile. You can switch from cutting 2-inch D2 tool steel to cutting ballistic glass. A few minutes later, you might slice thick neoprene rubber. This requires minimal to no machine reconfiguration. The operator simply changes the feed rate in the software. This flexibility allows contract shops to accept a much wider variety of jobs.
Production engineers must evaluate both technologies across strict performance dimensions. Abrasive jets excel in specific areas but fail in others. We need to define exactly where each technology belongs on the shop floor.
CNC milling dominates the ultra-high precision category. Rigid machine tools routinely hold tolerances between ±0.0001" and ±0.0005". These extreme tolerances are strictly required for aerospace mating surfaces. They are also necessary for press-fit bearings and hydraulic manifolds. You simply cannot achieve this precision with a jet of water and sand.
A standard Waterjet Cutting Machine generally holds tolerances around ±0.003" to ±0.005". The stream loses energy as it penetrates thick materials. This energy loss creates a phenomenon known as "taper." The cut develops a slight V-shape or barrel shape. However, modern 5-axis articulating cutting heads compensate for this geometry. They tilt the nozzle slightly to push the taper onto the scrap side of the cut.
We must define an absolute limitation here. Waterjets exist primarily for through-cutting. They cannot reliably machine flat-bottom blind pockets. You cannot use them to tap threads into a hole. They cannot face-mill a rough surface flat. They lack the depth control required for genuine 3D surfacing.
Milling centers excel at 3D machining. They use ball end mills to interpolate complex sweeping curves. They drill precisely controlled counterbores. If your part requires multiple internal features with specific depth callouts, a mill is mandatory.
Raw cutting speeds often favor the mill when working with soft materials like aluminum. A high-speed spindle rips through aluminum blocks much faster than a water stream. However, you must balance raw speed against total "art to part" time.
Waterjets require drastically less setup and fixturing time. You slap a plate onto the slats, weight it down, and press start. This yields much faster overall throughput for low-volume production runs. Prototyping happens in hours rather than days. For high-volume production of complex parts, the mill eventually overtakes the waterjet in efficiency.
Common Capability Comparison Chart
Feature/Capability | CNC Milling | Waterjet Cutting |
|---|---|---|
Standard Tolerance | ±0.0001" to ±0.0005" | ±0.003" to ±0.005" |
Blind Pockets & Threads | Excellent | Not Possible |
Thermal Distortion | High (requires coolant) | None (cold process) |
Material Utilization | Poor (wide chips/margins) | Excellent (narrow kerf) |
Setup Time | High (complex fixturing) | Low (flat plate weighting) |
Raw material costs dictate profitability in heavy fabrication. Utilizing every square inch of a metal plate directly increases your bottom line. Waterjet technology provides a massive financial advantage regarding material yield.
The system utilizes micro-joints and tight nesting software. The cutting stream possesses a very small kerf, typically measuring between 0.030" and 0.040". This narrow path allows programmers to nest parts merely millimeters apart on a single sheet. The CAM software generates micro-joints to hold the parts in place during the cut. This eliminates the need for bulky edge clamps.
Remnant recovery changes the return on investment equation. Traditional milling turns expensive stock into a bin of metal chips. You sell these chips to recyclers for pennies on the dollar. Waterjet cutting leaves usable, solid drop-pieces. You can save these internal cutouts for future jobs. When cutting expensive alloys like titanium or specialized stainless steel, remnant recovery saves thousands of dollars annually.
You also save money by eliminating secondary operations. Aggressive milling introduces mechanical stress into the part. Laser and plasma cutting introduce severe thermal stress. These methods often require expensive stress-relief cycles in an oven. They also require edge-hardening removal. Because water acts as a cold cutting process, the material retains its original molecular structure. You skip the annealing oven entirely.
Purchasing capital equipment requires transparent expectations. Sales brochures often gloss over the daily logistical challenges. We want you to understand the real-world operational demands of running this technology.
Consumables and abrasive management require dedicated logistical planning. You must purchase pallets of garnet abrasive constantly. You must store this heavy material in a dry environment. More importantly, you must dispose of the spent garnet. Cutting creates heavy, wet abrasive sludge in the catch tank. You need a reliable sludge removal system. You must also pay disposal fees to haul this heavy waste away.
Facility requirements go beyond floor space. A standard Waterjet Cutting Machine demands specific utilities. You need a footprint for water filtration and softening systems. Hard water destroys high-pressure pumps quickly. You need high-voltage electrical drops for the massive intensifier pumps. You must also implement ambient noise and moisture control in your shop. The cutting process gets loud and splashes dirty water.
Maintenance downtime is an unavoidable reality. You are dealing with ultra-high-pressure components. The seals, orifices, and mixing tubes experience extreme wear. They will fail. You must adhere to strict preventative maintenance schedules. Rebuilding an intensifier pump takes time and skill. If you ignore maintenance, you will experience catastrophic component failures during critical production runs.
Best Practices for Maintenance:
Test water quality monthly to ensure proper filtration.
Stock spare high-pressure seals and orifices on the shelf.
Rotate the mixing tube regularly to ensure even internal wear.
Evaluating your specific production mix helps you choose the right path. No single machine solves every manufacturing problem. Use this logical framework to guide your next capital investment.
Evaluate Volume and Geometry: Assess if your parts are mostly flat profiles or complex 3D blocks.
Analyze Material Costs: Determine how much money you lose annually to metal chips and scrap.
Review Tolerance Requirements: Check if your prints truly require ±0.001" or if ±0.005" is acceptable for the application.
You should stick to milling for specific workloads. High-volume production of complex parts demands a mill. If your parts require 3D contours, blind features, or tight-tolerance bores, keep them on the CNC center. If a part features dozens of threaded holes, milling remains the most efficient process.
You should switch to waterjet technology for profiling flat patterns. It dominates when cutting thick, thermally sensitive, or heavily abrasive materials. It proves especially profitable in low-to-medium volume mixes. Job shops that take on diverse materials benefit massively from the quick changeover times.
The hybrid approach represents the most common enterprise solution. Industry leaders practice "near-net shaping." They use a Waterjet Cutting Machine to rapidly cut blanks from plate stock. They nest these blanks tightly to save material. Then, operators move these near-net shapes to the CNC mill. The mill performs fast, light finishing passes on critical dimensions only. This maximizes raw material yield while maintaining aerospace tolerances.
We must reiterate our summary verdict clearly. A waterjet is rarely a direct 1:1 replacement for a multi-axis CNC mill. They serve fundamentally different geometric purposes. However, it represents a superior alternative for 2D profiling and maximizing raw material utilization. It thrives in high-mix, low-volume job shop environments.
Take action before making a capital investment. Conduct a part-cost analysis using your own CAD files. Compare the tooling and material scrap costs of milling against the abrasive costs of water cutting. Request a physical sample cut from an equipment manufacturer. Evaluate the edge quality and measure the real-world cycle times. Data-driven decisions guarantee a smoother transition and a faster return on your investment.
A: Compare hourly operating costs carefully. You must weigh waterjet garnet and power costs against CNC tooling and coolant. Waterjets often have higher hourly consumable costs. However, these are frequently offset by drastically lower setup times and significant reductions in raw material waste.
A: Yes. Waterjets easily cut hardened tool steels, ceramics, and titanium alloys. They accomplish this without the severe tool wear, heat generation, and heavy spindle load experienced in traditional milling.
A: Waterjets can practically cut metal plates up to 6–8 inches thick, or even more. Though the cutting speed drastically decreases and edge taper increases. Milling is strictly constrained by end mill length, tool deflection, and spindle rigidity.
A: The software and CAM barrier for 2D waterjet cutting is generally lower than multi-axis CNC milling. However, regular high-pressure machine maintenance and parameter troubleshooting still require distinct mechanical aptitude and technical skill.


